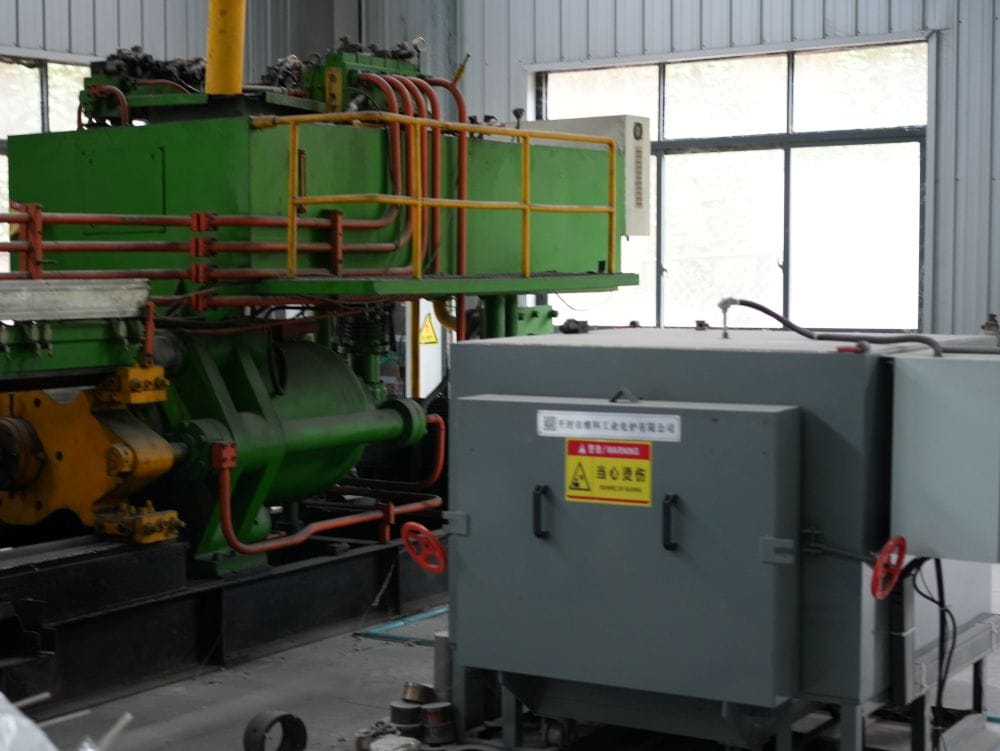
Magnesium tubes are used when a part needs a hollow section with low mass and useful stiffness for its weight. Common examples include aerospace and transport structures, equipment frames, electronics supports, sporting goods, and selected industrial assemblies. A tube is not chosen simply because magnesium is light. The load path, wall thickness, joining method, corrosion environment, and supply route have to work together before it becomes a sensible production part.
Most magnesium tubes are discussed as wrought extrusions, usually in a round, rectangular, square, or custom hollow profile. The hollow center removes weight while leaving material farther from the neutral axis, which can be a very efficient way to build bending stiffness. It is a practical shape when the same cross-section runs over a meaningful length.
Why a tube can be a better use of magnesium than a solid bar
Magnesium’s low density is the starting point. Pure magnesium has a reference density of about 1.74 g/cm³; aluminum is about 2.70 g/cm³ and iron about 7.85 g/cm³. Alloy grade and condition change the exact value, so these are useful comparisons rather than part-design guarantees.
| Reference material | Density at about room temperature, g/cm³ | What that means for a tube concept |
|---|---|---|
| Magnesium | 1.74 | Low mass where a hollow section can carry the load efficiently |
| Aluminum | 2.70 | A common lightweight benchmark with a broader supply base |
| Iron / steel | 7.85 | Higher mass for the same volume; section can often be made thinner |
*Reference densities for the elements are from the NIST material-constants table. A certified alloy tube should be designed from its own material data and mill certificate.*
For a bending member, material near the outside of the section does most of the work. That is why a thin-wall tube can be more useful than a solid round bar of the same mass. But the wall cannot be made arbitrarily thin. A tube that looks stiff in a simple beam calculation can dent during handling, buckle locally at a clamp, or distort when a machining operation opens one side.
Tube geometry also creates a clean route for wiring, fluid lines, fasteners, or nested components. In a lightweight instrument frame, that internal space may be nearly as valuable as the weight reduction. In another project, the opening only creates a difficult die and a harder inspection problem. The cross-section has to earn its complexity.
Where magnesium tubes are used
Lightweight frames, rails, and support members
Long members with the same section from end to end are natural candidates. A round tube, rectangular tube, channel-like hollow section, or box profile can be cut to length and then drilled or machined at the ends. These parts appear in equipment frames, portable instruments, housings, guards, mounts, and noncritical structural supports where reducing carried weight is useful.
The decision is usually more specific than “make it lighter.” A portable unit may need an outer frame that is easy to lift but still stiff enough to protect internal electronics. A tube may place material in the right locations without turning the whole component into a heavily machined block.
Aerospace and transportation components
Aerospace and transportation programs have a long history of evaluating magnesium where mass reduction is important. In a tube application, the part may act as a support, a seat or cabin substructure, a cover-frame member, a duct-adjacent support, or a lightweight assembly element.
The application label alone is not enough to select material. Aerospace parts often bring requirements for flammability, corrosion exposure, coating, traceability, repair, and qualification. Vehicle parts may add vibration, road salt, stone impact, and joining to aluminum or steel. Those requirements can rule out an otherwise attractive tube design.
Sporting and portable equipment
Tube sections make sense in products that are carried, moved, or accelerated often. Handles, lightweight supports, camera or instrument structures, mobility equipment, and specialized sporting assemblies are examples where a hollow magnesium section can be evaluated.
Here, surface appearance can matter as much as basic strength. A small scratch or clamp mark may be acceptable inside industrial equipment but unacceptable on a consumer-facing product. Put the cosmetic zones on the drawing early. Coating, racking, edge finishing, and packaging are easier to plan before a profile is approved.
Industrial equipment and custom machine assemblies
Magnesium tubes are also used as a route to custom hollow profiles for industrial products. A profile may incorporate mounting lands, a cable channel, a protected cavity, or a stiffened outer wall. Extrusion can reduce the number of separate brackets or fasteners in a long assembly.
This route is most useful when the section repeats. A one-off body with a different shape every few inches is usually a machining, casting, fabrication, or assembly problem instead. The extrusion die pays back when the profile is stable and the quantity supports it.
The alloy and the tube route matter
AZ31B is a common starting point for extruded magnesium tube and general wrought work. It is often considered where formability and a practical supply route matter. AZ61A is usually brought in when an extruded section needs more strength, with the tradeoff that post-extrusion forming becomes less forgiving.
The table below is not a substitute for a specification. It is a way to begin the conversation with the right material family.
| Starting point | When it is commonly reviewed | Question to settle before ordering |
|---|---|---|
| AZ31B extruded tube | General lightweight tube, formed or machined section, moderate-strength structure | Will the tube be bent, expanded, flattened, or welded after extrusion? |
| AZ61A hollow extrusion | Higher-strength rails, sections, and tube-like profiles | Is the added strength more valuable than easier secondary forming? |
| Custom magnesium profile | Repeating section with ribs, mounting faces, or internal features | Can the walls, corners, cavities, and straightness requirement be produced as one profile? |
For an alloy comparison, see AZ31B vs. AZ61A magnesium alloy. If the project is already centered on a long hollow profile, our AZ61A magnesium extrusion guide covers section design, walls, straightening, machining, joining, and coating in more detail.
Seamless extruded tube and welded tube should not be treated as interchangeable in the drawing. The weld area, wall thickness, dimensional requirements, pressure duty, forming operation, and inspection method can change the decision. A tube used as a cosmetic support is a very different part from a tube that must carry pressure or seal fluid. For pressure-containing service, involve the responsible design and compliance team before choosing a magnesium alloy route.
Design details that decide whether the tube stays straight
Tube designers often focus on outside diameter and wall thickness first. Those matter, but the next questions are usually where the trouble starts: How will it be held during machining? Where can a hole be drilled without crushing or distorting the section? Does a thread need enough wall behind it? Is the tube open at both ends or capped during assembly?
A common problem is cutting a window into one side of a thin tube. The tube can lose stiffness, release residual stress, and move after unclamping. The machining shop may need soft jaws, an internal mandrel, a sacrificial support, or a staged machining sequence. These are manageable choices, but they should not be discovered after the extrusion order is placed.
Keep wall transitions gradual where possible. Use radii instead of demanding sharp internal corners in a custom profile. If a very crisp interface is required for a mating component, it may be better to leave material in the extrusion and finish-machine that feature.
Long tubes also bring straightness and twist into the conversation. A supplier needs the overall length, critical straightness zone, datum faces, and any post-extrusion straightening or machining requirements. “Must be straight” is not a measurable purchasing instruction. State the allowed deviation, how it will be supported during measurement, and whether the requirement applies before or after cutting.
Machining, joining, and corrosion protection
Extrusion rarely eliminates machining. End faces may be trimmed, holes drilled, threads cut, mounting lands milled, or local features finished to a tighter tolerance. The best profile leaves machining allowance only where it earns its keep. Adding a large flat pad everywhere because one end needs a threaded insert adds material and press complexity to every foot of extrusion.
Magnesium chips need their own shop controls. A supplier should understand the alloy, chip size, collection method, housekeeping, coolant or cutting-fluid plan, and fire-safety procedures before machining begins. This is especially important with deep holes, thin walls, and small features that generate fine chips. Magnesium alloy CNC machining is a separate process review, not a standard afterthought.
Joining requires the same care. Mechanical fasteners, adhesive bonding, welding, inserts, and contact with dissimilar metals each have different corrosion and distortion concerns. A stainless fastener or aluminum bracket may be entirely workable, but the joint design, isolation method, coating system, and service environment need to be specified as a group.
Magnesium does not get a free pass on corrosion because the part is indoors. Condensation, salt, cleaning chemicals, crevices, scratches, and a coating break at a fastener can all matter. The appropriate surface treatment depends on the alloy, environment, finish requirement, and later assembly steps. Ask for the coating route and masking plan with the tube quote, not after the holes are drilled.
When a magnesium tube is not the best answer
There are cases where another route is simpler. If the part has a highly variable cross-section, a casting or fabricated assembly may be more logical. If it needs extensive room-temperature forming after production, a different alloy or another material family may be easier to work with. If the design needs a tiny quantity of a complex custom section, machining from stock may avoid the cost and lead time of an extrusion die.
Aluminum is often the first alternative because tube, pipe, and profile availability is broad. Steel may remain the better option when local dent resistance, joining familiarity, low material price, or a known coating system outweigh mass reduction. The right comparison includes the whole assembly. A magnesium tube can remove enough weight or parts to justify itself; it can also introduce supply and finishing work that a simple aluminum section avoids.
Before requesting a quote, send the section view, material preference, length, wall target, straightness or twist requirement, load direction, machining features, joining plan, coating environment, quantity, and whether the tube is decorative, structural, or pressure-related. That short project description gives the supplier a much better starting point than an outside diameter and a broad request for “magnesium tubing.”