EV31A magnesium alloy is a rare-earth-containing magnesium casting alloy used when low weight has to coexist with reliable strength at moderately elevated temperature. It is most often specified for sand castings, commonly in a T6 condition. EV31A is not a general replacement for AZ91 or a default choice for every lightweight part. It makes more sense when the service temperature, casting route, and required performance justify a specialty alloy and its tighter supply route.
For product forms, custom sizes, and material inquiry support, see our EV31A magnesium alloy page. This article is for the early material decision, before a drawing is released for tooling or machining.
Where EV31A fits
EV31A is generally discussed in the magnesium casting family, not as a standard wrought plate or extrusion grade. The alloy uses neodymium, gadolinium, zinc, and zirconium additions. That chemistry supports a property balance different from common aluminum-containing magnesium casting alloys.
In practice, EV31A comes up when an engineer has a cast structural housing, bracket, cover, or support component that needs to stay light and is expected to see more heat than an ordinary room-temperature part. Aerospace and specialty transportation projects are typical places to start the conversation, but the alloy should be selected on the actual duty cycle, not the industry label on the purchase order.
The part shape still matters. A thick sand-cast housing, a thin ribbed wall, and a local machined bore do not cool at the same rate or respond to heat treatment in the same way. Good castings begin with the alloy, but they do not end there. Section thickness, gating, feed, heat treatment, and the machining allowance all show up in the finished part.
Chemistry and property data
EV31A is commonly identified as a Mg–Nd–Gd–Zn–Zr rare-earth alloy. The alloy designation associated with SAE AMS4429 describes a nominal composition of approximately 2.8% neodymium, 1.4% gadolinium, 0.4% zinc, and 0.6% zirconium, with magnesium as the balance. Production certification should always be checked against the purchase specification, not against nominal chemistry alone.
| Element or condition | Practical reference point |
|---|---|
| Magnesium | Balance |
| Neodymium (Nd) | About 2.8% nominal |
| Gadolinium (Gd) | About 1.4% nominal |
| Zinc (Zn) | About 0.4% nominal |
| Zirconium (Zr) | About 0.6% nominal |
| Common delivery route | Sand casting, often solution treated and artificially aged (T6) |
The table is an alloy identity guide, not a material certificate. Chemistry limits, impurity limits, casting class, test-bar location, and heat treatment must follow the standard or customer specification named on the order.
Mechanical values need the same care. ASTM B80 and AMS4429 references are tied to sand castings and a defined T6 treatment, not to a generic EV31A block or a machined part of any thickness. Published minimum values for EV31A-T6 sand castings are commonly shown as 248 MPa tensile strength, 145 MPa 0.2% proof strength, and 2% elongation. Those figures give a sensible first screen; they are not a blanket promise for every casting geometry.
| EV31A-T6 sand-casting reference | Published minimum value* |
|---|---|
| Ultimate tensile strength | 248 MPa (36 ksi) |
| 0.2% proof / yield strength | 145 MPa (21 ksi) |
| Elongation | 2% |
*Use the applicable material specification, casting quality level, and supplier test report for acceptance. Section size, location, and process route influence the properties achieved in a real component.
T6 heat treatment is part of the material route, not just a suffix added to the drawing. Solution treatment, quenching, and artificial aging affect precipitation and strength. They can also leave a casting needing careful fixturing during finish machining, particularly when thin walls or broad machined faces are involved.
Casting and finishing the part
EV31A is usually a sand-casting conversation. Sand casting can make sense when the component is too complex or too thick for a straightforward machined blank, and annual volume does not favor a permanent die route. It can also leave useful stock for machining datum faces, bores, threads, and sealing surfaces after the casting is stabilized.
This is not a reason to call every feature “as-cast.” A sealing face may need machining. A bore that controls alignment may need finish machining. A threaded hole almost certainly needs a clear machining plan. Put those requirements on the drawing early, along with the surfaces that must remain as-cast and any cosmetic expectation.
Gating and feeding need to match the section map. Thick regions need a sound feed path. Thin ribs need a fill path that does not freeze before the cavity is complete. A casting supplier may ask for a model, not just a 2D print, because that is where hot spots, machining allowance, and tool access become visible.
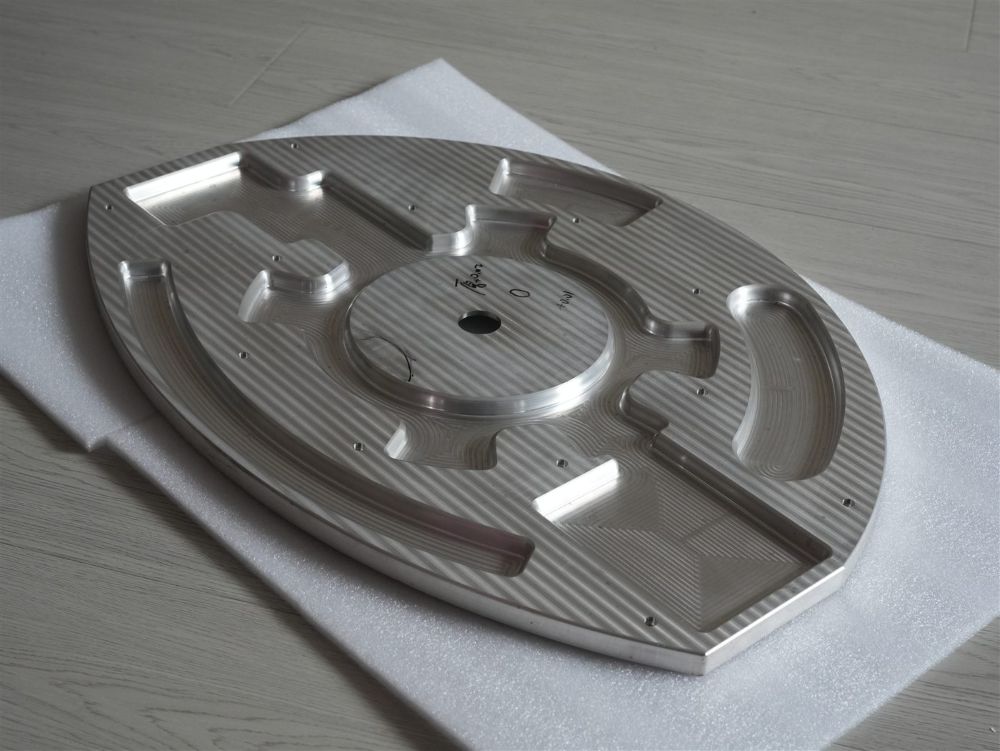
After casting and heat treatment, EV31A can be machined, but it should not be treated as an ordinary stock block with no history. Confirm the casting condition, datum strategy, remaining wall thickness, and required free-state inspection. Magnesium machining also requires responsible chip handling and housekeeping. Our magnesium alloy CNC machining guide covers those practical controls.
When a supplier posts the machining program, the controller and machine configuration still matter. Tool paths are built around the fixture, tool reach, coolant arrangement, and the actual machine—not copied blindly between shops. For a plain-language explanation, read G-code vs. M-code and what each CNC command controls.
Service temperature, corrosion, and joining
EV31A is often considered because rare-earth additions can support elevated-temperature capability relative to many common magnesium cast alloys. “Elevated temperature” still needs a number. A short excursion, a constant soak, a cyclic thermal load, and a component next to an engine or electronics heat source are not equivalent service conditions.
Ask the design team to state the maximum metal temperature, duration at temperature, load type, and number of cycles. If creep, fatigue, or distortion is important, those requirements should be reviewed against a qualified property source for the exact condition. Room-temperature tensile values alone are not enough.
Corrosion protection should be decided with the assembly, not after the casting is already approved. Magnesium needs sensible surface treatment and attention to moisture traps, dissimilar-metal contact, fasteners, and coating damage. A protected interior housing in a controlled environment is a very different job from an externally exposed component that will see salt, condensate, or repeated washdown.
Joining needs equally specific planning. A machined bolted interface may be the simplest path. Welding, adhesive bonding, inserts, and threaded features all change the local design and may affect finish selection. State which surfaces must remain conductive, which are cosmetic, and which must be sealed.
When EV31A is worth considering
EV31A is worth a closer look when a component is genuinely casting-led, weight-sensitive, and expected to operate in a temperature range where a standard magnesium grade needs more scrutiny. Examples may include specialized housings, structural supports, covers, and equipment components with a defined heat exposure and a clear route for corrosion protection.
It is usually not the first material to quote when the part is simply a flat machined plate, a basic extrusion, or a low-temperature casting with ordinary property requirements. In those situations, a more common alloy and stock form may offer better availability, lower material cost, and a simpler manufacturing path.
The best comparison is not “Is EV31A stronger than another grade?” It is “Does this part need the specific temperature and casting behavior EV31A was chosen for?” If the answer is uncertain, start with the part function, production quantity, service environment, and available process routes. Our broader magnesium alloy selection guide can help frame that review.
What to clarify before requesting EV31A
An accurate inquiry does not need to be long. A 3D model, 2D drawing, alloy and condition, expected quantity, target casting process, key machined surfaces, service temperature, coating, and inspection requirements give the supplier enough to begin a useful conversation.
If the part already has a material specification, include it. If it does not, explain the load, temperature, environment, and acceptance criteria rather than asking the supplier to infer them from a photograph. That is usually the fastest way to find out whether EV31A is appropriate—or whether another magnesium route is more practical.
Questions about EV31A magnesium alloy
Is EV31A a cast or wrought magnesium alloy?
EV31A is commonly specified as a magnesium sand-casting alloy. Confirm the required product form and specification before sourcing because it should not be assumed to be interchangeable with a wrought plate, extrusion, or forging grade.
What does T6 mean for EV31A?
T6 refers to a solution-treated and artificially aged condition. The exact cycle and acceptance requirements should follow the applicable material specification, not a generic online description.
Can EV31A be CNC machined?
Yes, cast EV31A components can be finish machined where the design needs controlled datums, bores, threads, or sealing faces. The supplier should plan workholding and magnesium chip management around the casting geometry.
Is EV31A suitable for high-temperature service?
It may be considered for elevated-temperature applications, but the decision needs the actual metal temperature, time at temperature, load, and required mechanical behavior. A room-temperature tensile table is not enough to qualify a high-temperature part.
Does EV31A need corrosion protection?
In most real assemblies, surface protection and joint design need review. The appropriate treatment depends on the service environment, mating materials, exposed surfaces, and performance requirements.